
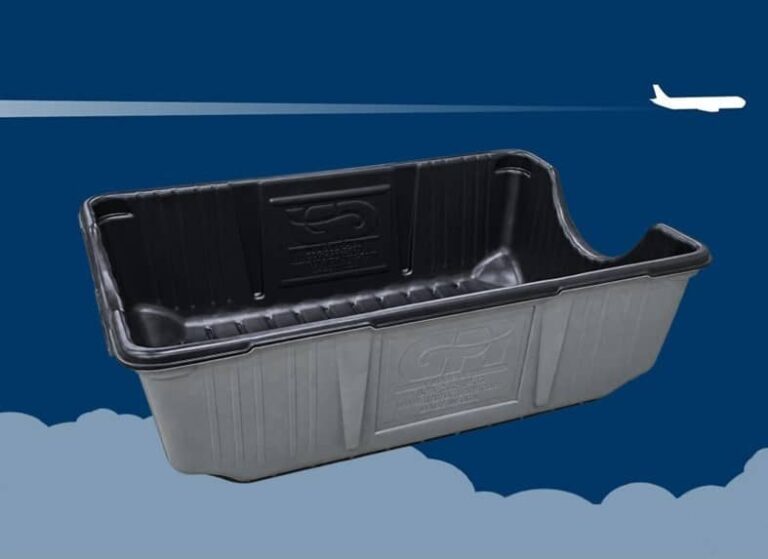
For airlines and airports sourcing baggage handling tubs, the container itself is only part of the equation.
The choice of manufacturer matters too. Selecting a partner with proven technical expertise can help maintain reliable day-to-day operations over the life of the product.
At Greenwood Plastics Industries (GPI), we manufacture baggage handling tubs for major aviation organizations across the country.
Our experience has given us a firsthand understanding of how fabrication methods, quality control, and production capabilities contribute to a superior finished product.
Here are a few considerations to keep in mind when evaluating potential manufacturers.
Precision Starts With the Process
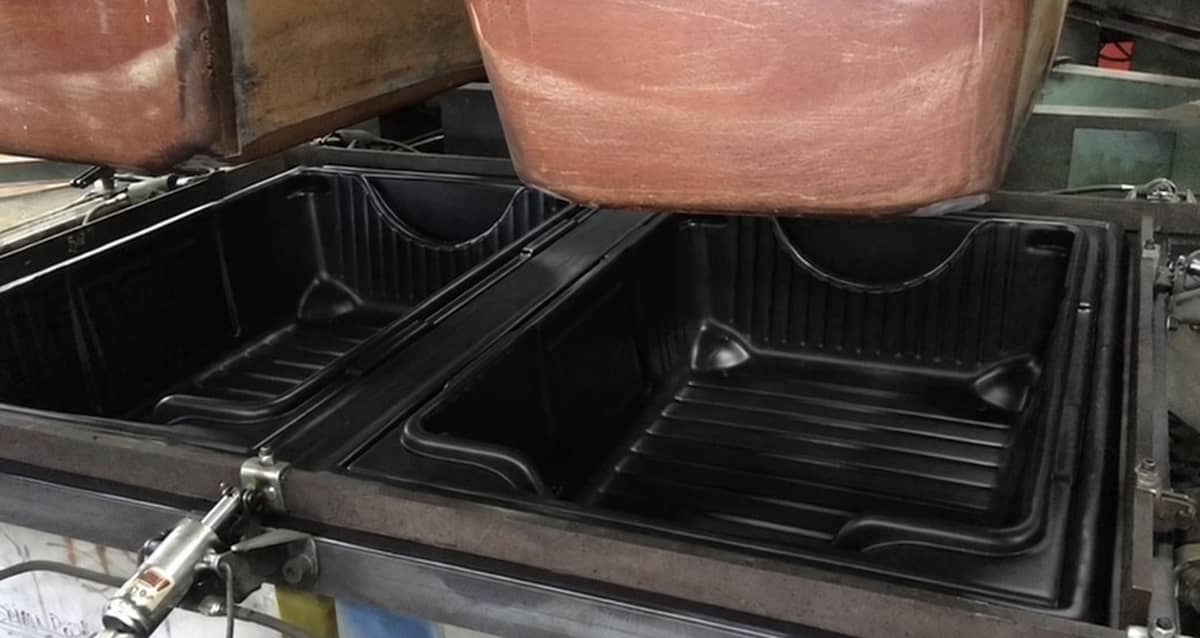
Airline baggage handling tubs have a relatively straightforward design, which places greater emphasis on precision during production.
Even small variations in dimensions or shape can affect how well tubs nest together, stabilize contents during transport, and interact with an existing baggage handling system. Effective process control is essential from the start to support smooth throughput at high-volume transfer points.
Part of what sets GPI apart is that our tubs are manufactured using a three-station thermoforming machine with dedicated heating, forming, and cooling stages. Systematic monitoring throughout each phase of production helps ensure that each product meets the same criteria for fit, minimizing variations from one tub to the next.
Design Features & Benefits Play a Role
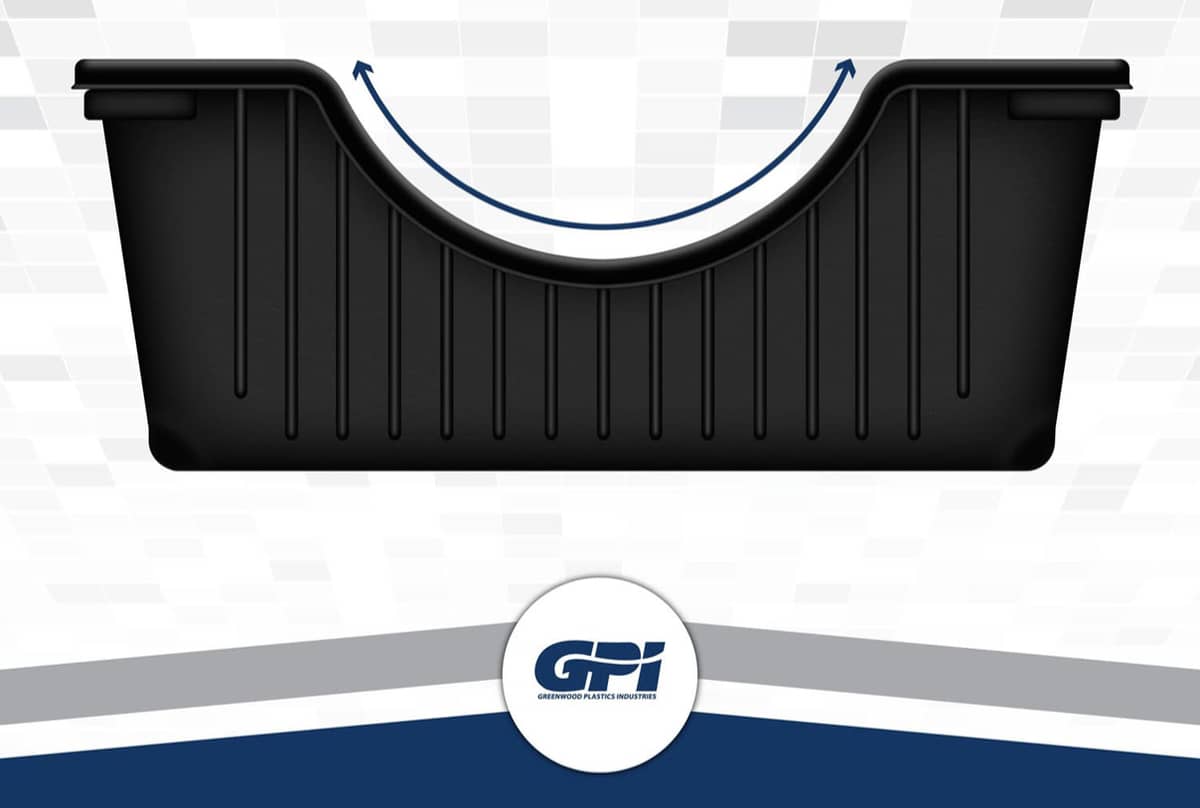
While airline baggage tubs share many common design characteristics, their specifications can vary based on the intended function.
Differences in handling equipment, facility layouts, and intended use may call for modifications to standard designs. Considerations that might seem relatively minor can affect how smoothly tubs move through baggage handling systems.
Design features found in GPI’s baggage handling tubs serve specific purposes:
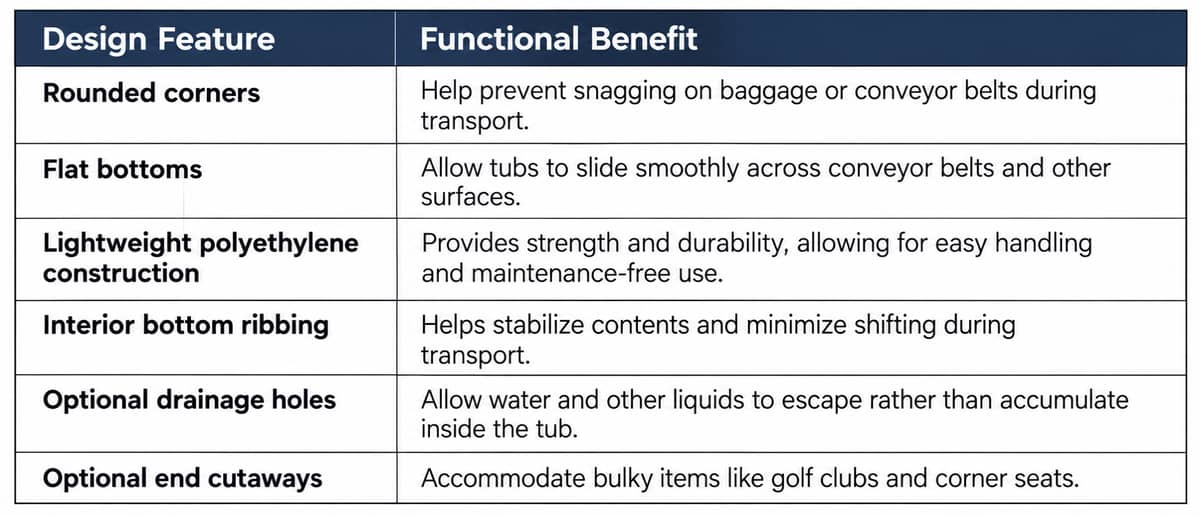
A manufacturer should have the capability to accommodate these requirements while ensuring the finished tubs perform reliably within the systems they’re designed to serve.
Reliable Production Across Multiple Orders
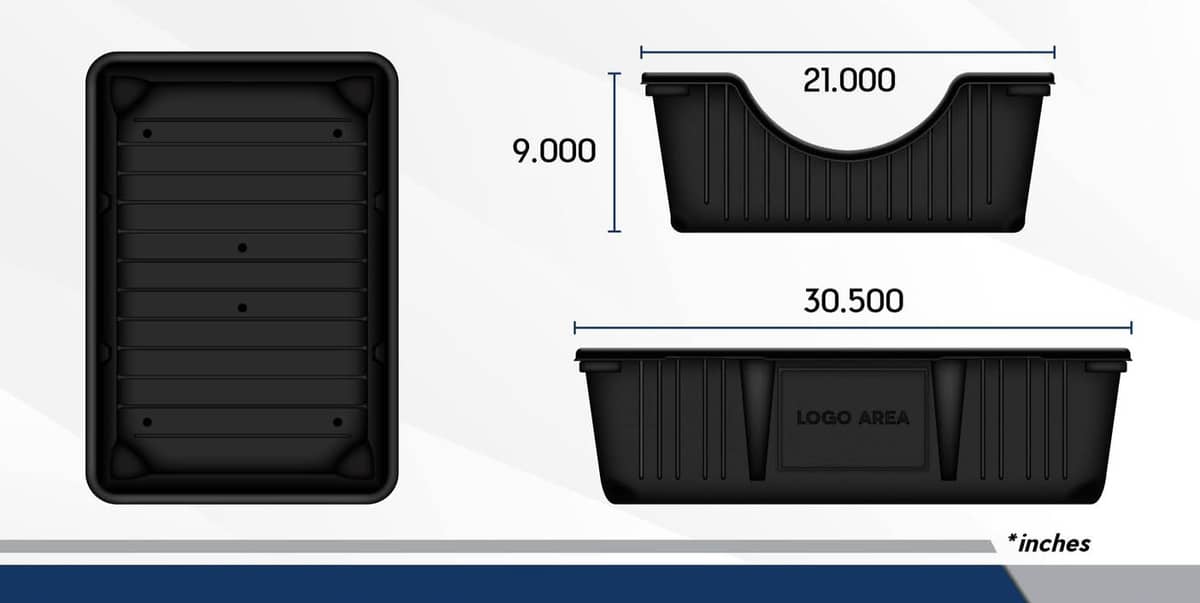
Baggage handling tubs are often purchased in large quantities, with additional orders placed as customers’ needs evolve.
Whether ordering an initial supply or replenishing an existing fleet, customers should be able to expect the same dimensions, material specifications, and overall construction from one order to the next.
Uniform results across successive runs help simplify inventory management and reduce the need for adjustments in the field. A manufacturer’s ability to meet those expectations reflects its production capabilities and commitment to sustained reliability.
Customization Adds Value
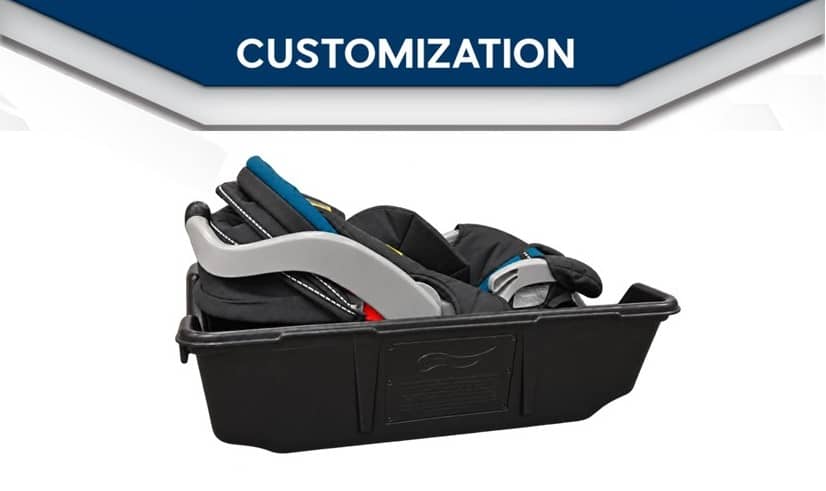
Customization often serves a practical purpose beyond appearance alone.
GPI offers airline logos, airport or terminal identification, custom colors, and two-tone designs. These options can help distinguish tubs by airline, hub, terminal, location, or intended use. Clear visual cues make it easier for ground staff to route units correctly during peak periods.
For larger operations, visual identification provides a way to organize equipment while also maintaining brand awareness.
Looking Beyond the Manufacturing Floor
A manufacturer’s familiarity with the baggage handling industry can add another layer of value.
As a member of the International Association of Baggage System Companies (IABSC), GPI stays engaged with the broader aviation community.
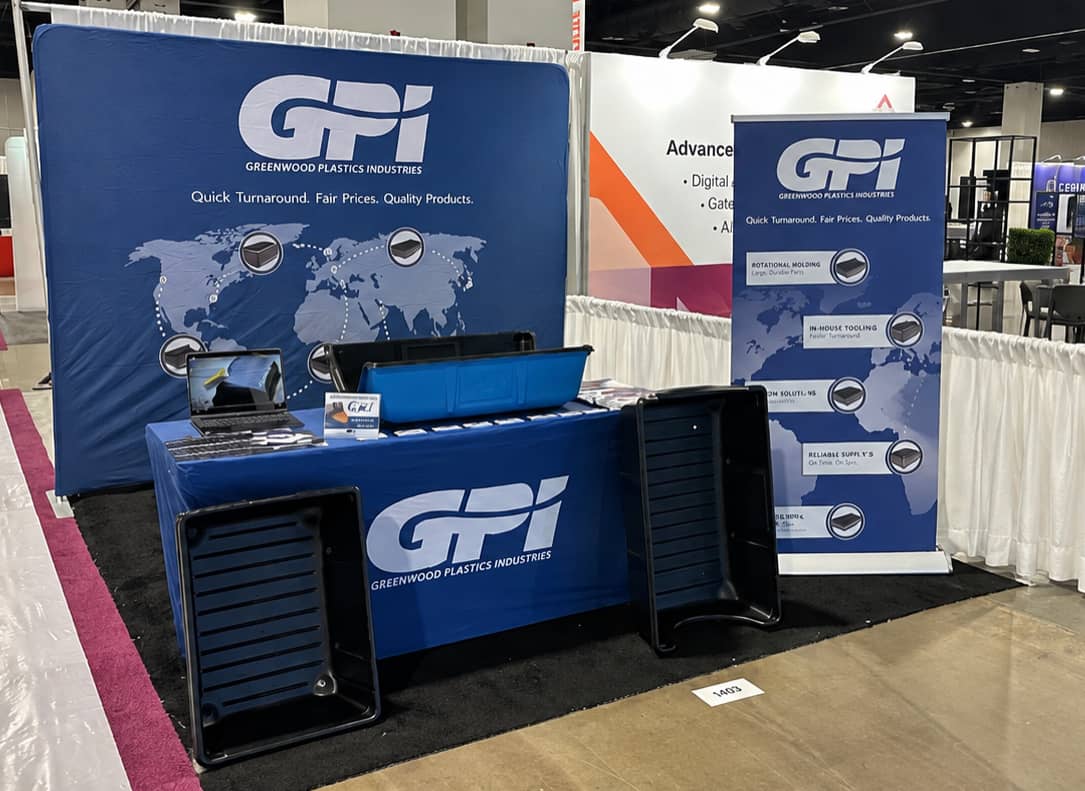
Our industry involvement has also included participation in the American Association of Airport Executives (AAAE) Annual Conference & Exposition, providing a chance to connect with aviation professionals and gain additional insight into airport operations.
These connections help us maintain relationships throughout the baggage handling sector while staying close to the people and environments our products serve. Ongoing dialogue with operators also offers an opportunity to gather practical feedback that can inform future product refinements.
Choosing the Right Manufacturer
The differences between airline baggage handling tubs may not always be apparent from the completed product alone.
Often, the real differences come down to manufacturing quality, how well the materials and design suit the application, and the supplier’s ability to meet customer needs over time. Some of GPI’s baggage handling tubs have remained in service for decades, reflecting the importance of durability and long-term performance. A supplier that takes a long-term approach to customer relationships is better positioned to provide consistent support as those needs evolve.
With thermoforming expertise and experience serving the aviation industry, GPI understands the manufacturing requirements behind dependable baggage handling tubs. We bring that knowledge to every project, helping airlines and airports find solutions suited to their operations.